

Pumping heat transfer fluids (HTF), thermal oils, and aggressive chemicals at temperatures exceeding 300°C places extraordinary mechanical stress on fluid handling equipment. In these extreme environments, fluid containment is the primary engineering objective. Traditional dynamic sealing methods, such as single or double mechanical seals, inevitably degrade under continuous thermal cycling, leading to fugitive emissions, costly maintenance downtime, and severe fire hazards when handling combustible thermal oils. The structural solution to these vulnerabilities is the sealless magnetic drive pump. By replacing the physical drive shaft with a synchronized magnetic coupling, these pumps establish a hermetic pressure boundary that completely isolates the process fluid from the external environment. This engineering guide examines the mechanics of high-temperature magnetic drive systems, the metallurgical requirements for sustained high-heat operation, internal thermal management, and the hydraulic criteria for selecting the correct pump architecture.
The Mechanics of Sealless Magnetic Coupling in High Heat
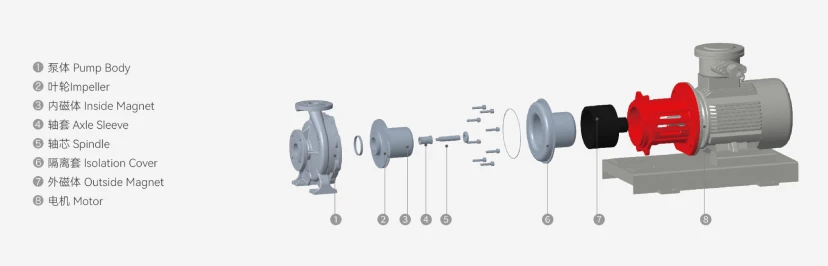
The fundamental architecture of a magnetic drive pump separates the driving power from the wetted pumping mechanism. The system consists of three primary drive components: the outer magnetic rotor attached to the motor shaft, the inner magnetic rotor attached to the pump impeller, and the isolation sleeve (containment shell) that sits securely between them. As the motor turns the outer rotor, the magnetic flux penetrates the stationary isolation sleeve, locking onto the inner rotor and transmitting torque synchronously.
This configuration converts the dynamic rotary seal into a static seal. In high-temperature applications, this distinction is critical. Mechanical seals rely on highly polished carbon, silicon carbide, or tungsten carbide faces pressed together by springs, with secondary elastomer O-rings providing the static boundary on the shaft. At temperatures approaching 400°C, these elastomers lose their elasticity, become brittle, or thermally degrade. Furthermore, high-temperature thermal oils often experience localized coking—the formation of hard carbon deposits—when exposed to atmospheric oxygen at the mechanical seal faces. This coking rapidly destroys the polished seal faces, causing sudden and catastrophic leakage. The magnetic drive architecture entirely eliminates the shaft penetration and the associated elastomers, resolving the root cause of high-temperature pump failures.
Metallurgical and Material Science for 400°C Operation
Operating at extreme temperatures requires precise material selection across all internal components. Standard magnetic drive pumps designed for water or ambient chemical transfer typically utilize Neodymium-Iron-Boron (NdFeB) magnets. While powerful, Neodymium magnets have a relatively low Curie temperature and begin to suffer irreversible demagnetization at temperatures above 150°C.
For high-temperature magnetic drive pumps, engineers specify Samarium-Cobalt (SmCo) rare-earth magnets. Specifically, the Sm2Co17 alloy maintains robust magnetic coercivity and flux density at continuous operating temperatures up to 350°C, and specialized grades can operate safely at 400°C. This ensures that the torque transmission remains locked without slipping, even under maximum hydraulic load and extreme thermal expansion.
The isolation sleeve must withstand the system pressure while remaining thin enough to maximize magnetic coupling efficiency. In high-temperature thermal oil systems, the sleeve is typically manufactured from Hastelloy C-276, Titanium, or 316L stainless steel. Hastelloy C-276 is frequently selected not just for its corrosion resistance, but for its high electrical resistivity. As the magnetic field rotates through the metallic sleeve, it induces electrical eddy currents, which generate localized heat. Materials with high electrical resistivity minimize these eddy current losses, preventing unnecessary heat addition to the thermal fluid and protecting the SmCo magnets from exceeding their thermal limits.
Sintered Silicon Carbide Bearing Systems
Because the inner rotor and impeller shaft are entirely enclosed within the containment shell, they must be supported by internal bearings lubricated by the pumped medium. Standard ball bearings or oil-bath lubrication cannot be utilized. Instead, high-temperature magnetic drive pumps rely on hydrodynamic plain journal bearings and thrust washers.
Sintered Silicon Carbide (SSiC) is the industry standard for these internal wetted bearings. SSiC provides exceptional hardness, ranking just below diamond, which offers superior wear resistance against any particulate matter suspended in the thermal oil. More importantly for high-temperature applications, SSiC has a very low coefficient of thermal expansion and outstanding thermal conductivity. This allows the bearings to maintain the precise dimensional clearances required for hydrodynamic lubrication across a temperature gradient from ambient startup to a 400°C operating state, without seizing or fracturing from thermal shock.
Internal Thermal Management and Cooling Flow Paths
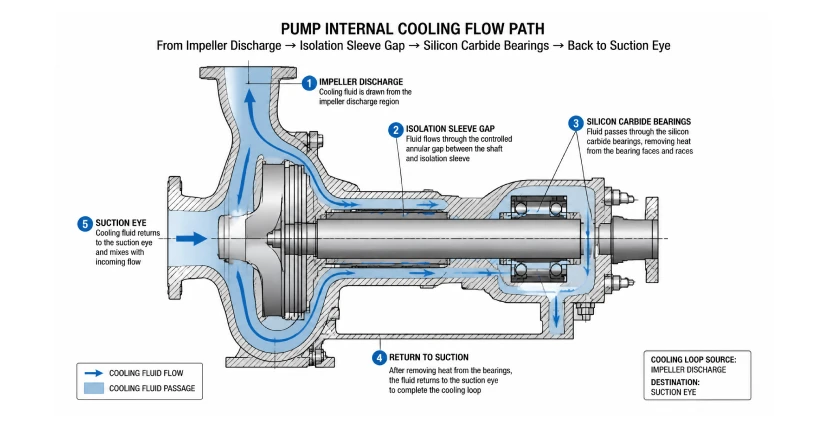
The reliability of a high-temperature magnetic drive pump depends heavily on its internal fluid dynamics. The internal bearings require a continuous flow of the pumped medium to establish the hydrodynamic film that prevents metal-to-metal contact. Simultaneously, this fluid flow acts as a coolant to dissipate the heat generated by the eddy currents in the isolation sleeve.
Engineers design a dedicated self-circulating flow path within the pump casing. A small percentage of the high-pressure fluid discharged from the impeller is routed behind the impeller, passing through the annular gap between the inner magnet and the isolation sleeve, flowing through the silicon carbide journal bearings, and finally returning to the low-pressure suction eye of the impeller.
In extremely high-temperature applications, careful management of this internal flow is vital. If the fluid flow is insufficient, the localized heat from the eddy currents can cause the thermal oil to reach its cracking temperature, leading to fluid degradation, vapor locking, and immediate bearing failure due to dry running. Advanced pump designs precisely calibrate these internal clearances to ensure a high-velocity flush that rapidly removes heat while maintaining system pressure.
Thermal Decoupling from the Drive Motor
While the internal pump components are rated for 400°C, the external electric motor and its standard rolling-element bearings are typically rated for ambient environments (up to 40°C or 50°C). Transferring 400°C fluid creates a massive thermal gradient along the pump structure. High-temperature magnetic drive pumps utilize an extended intermediate bracket equipped with exterior cooling fins. This physical separation and increased surface area allow ambient air to dissipate the conducted heat before it reaches the motor flange, protecting the motor bearings and stator windings without the complexity and maintenance burden of external water-cooling jackets.
Vortex vs. Centrifugal Geometries for High-Temperature Service
High-temperature fluid transfer occurs in vastly different operational scales, dictating the choice between centrifugal and vortex pump geometries.
Centrifugal magnetic drive pumps are deployed in large-scale heat transfer networks, primary boiler circulation, and bulk chemical heating. They excel in delivering high volumetric flow rates at low to moderate differential pressures. Their impeller design is highly efficient for continuous, bulk transfer where the primary requirement is moving large masses of thermal energy quickly.
Conversely, precision industrial applications often require a different hydraulic profile: very high differential pressure at relatively low flow rates. This is the domain of the vortex pump. Using a regenerative peripheral impeller, a vortex pump imparts kinetic energy to the fluid multiple times within a single revolution, achieving differential heads that would require a complex, multi-stage centrifugal pump.
| Hydraulic Architecture | Primary Application | Flow Profile | Head Output | Gas Handling |
|---|---|---|---|---|
| Centrifugal Magnetic Drive | Bulk thermal oil transfer, primary boiler loops | High | Low to Medium | Poor (< 5% entrained gas) |
| Vortex Magnetic Drive | Precision TCUs, semiconductor cooling modules | Low to Medium | Extremely High | Excellent (up to 20% gas) |
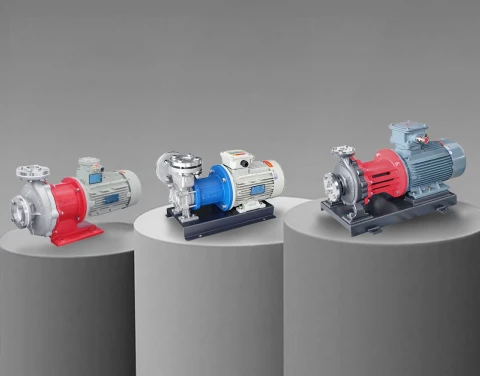
In specialized sectors such as semiconductor manufacturing, lithium battery separator coating, and medical device temperature control, compact high-head performance is critical. Equipment like CMP conditioning units, CVD/PVD thin-film deposition tools, and dedicated Temperature Control Units (TCUs) utilize compact vortex magnetic drive pumps. The Aulank MDH and MDW series, engineered with sealless vortex hydraulics, provide the strict parameter control and zero-leakage assurance required for these advanced manufacturing environments. Furthermore, vortex pumps can handle up to 20% entrained gas without vapor locking, providing crucial resilience against localized fluid flashing or off-gassing at extreme temperatures.
Operational Safeguards and System Integration
To guarantee the longevity of a high-temperature magnetic drive pump, system engineers must implement specific operational safeguards. The primary vulnerability of any sealless pump is dry running. Without fluid to lubricate and cool the SSiC bearings, frictional heat will cause catastrophic bearing fracture within seconds.
System integration must include strict Net Positive Suction Head available (NPSHa) calculations to prevent cavitation. Thermal oils have specific vapor pressures that shift aggressively with temperature. Ensuring proper system pressurization prevents the heat transfer fluid from boiling at the pump suction. Additionally, active power monitoring on the motor drive is essential. A sudden drop in power draw instantly indicates a loss of fluid or cavitation, allowing the control system to shut down the pump before bearing damage occurs. Finally, high-temperature loops must utilize commissioning strainers to remove welding slag and construction debris, which can easily block the tight internal circulation paths of the magnetic drive.
Conclusion
The transition from mechanically sealed pumps to magnetic drive architectures in high-temperature applications represents a shift from reactive maintenance to proactive risk elimination. By completely removing the dynamic shaft seal, process facilities eradicate the primary source of thermal fluid leakage, associated fire risks, and unpredictable downtime. Whether utilizing high-flow centrifugal models for bulk heating or compact vortex models for precision semiconductor thermal control, selecting a pump engineered with Samarium-Cobalt magnets, optimized internal cooling paths, and sintered silicon carbide bearings ensures decades of stable, zero-leakage operation under the most demanding thermal conditions.
Engineered Fluid Solutions with Aulank Pump
Aulank Pump manufactures specialized industrial fluid transfer solutions, focusing on zero-leakage, high-performance architectures. Our portfolio includes the MDS, MDH, and MDW series vortex magnetic drive pumps, engineered specifically for extreme temperature operations spanning -196°C to +400°C. Trusted by global leaders in semiconductor manufacturing, lithium battery production, and precision thermal control, Aulank delivers structural stability, customized motor configurations, and rigorous helium leak-testing for the most critical process environments. Whether you require an MDP Permanent-Magnet Canned Vortex Magnetic Drive Pump for compact integration or a high-capacity centrifugal unit, our engineering team provides precise sizing and metallurgical selection. Contact us today to secure the reliability of your advanced thermal systems.